Industrial Belt Conveyor

Industrial Belt Conveyor Manufacturers in Pune - S Cube Engineering
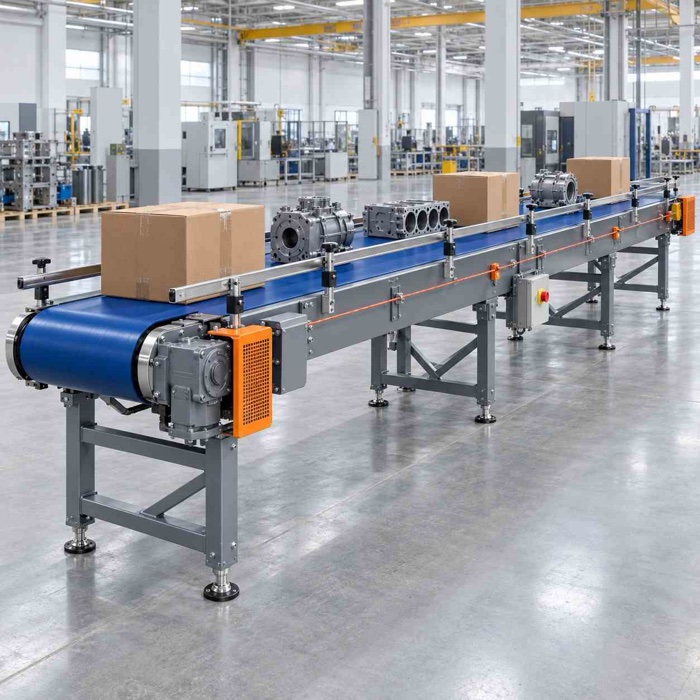
S Cube Engineering & Automation is trusted Industrial Belt Conveyor Manufacturers, Suppliers, Dealers and Exporters in Pune, Maharashtra. We deliver conveyor and industrial automation solutions engineered according to practical manufacturing and material-handling requirements.
Our Industrial Belt Conveyor solutions are developed with sturdy construction, stable operation and economical engineering to ensure dependable movement of materials. We provide customized conveyor arrangements based on belt selection, dimensions, load requirements, operating speed and application conditions, including Belt Conveyor Custom Designed Transport System for Industrial Manufacturing applications.
Our solutions are suitable for manufacturing, packaging, assembly, warehousing and various other industrial sectors. We emphasize appropriate technical design, quality manufacturing and responsive service to support efficient material handling, better production flow and reliable long-term conveyor performance.
What Is an Industrial Belt Conveyor and How Does a Belt Conveyor System Work?
An Industrial Belt Conveyor is a powered conveying equipment system used to continuously transfer products, components, packages or bulk materials from one location to another. It consists of a continuously moving belt arranged over a supporting structure with rollers and pulleys. This makes it an efficient material handling system for manufacturing, assembly, packaging, logistics and warehouse applications.
Working Principle of Industrial Belt Conveyor
An Industrial Belt Conveyor operates by continuously rotating the belt with the help of a motor-driven pulley, enabling materials to travel steadily between predetermined points.
- Power Transmission: The electric motor supplies rotational power through a gearbox to the drive pulley, which moves the conveyor belt.
- Friction Drive: Movement is transmitted from the drive pulley to the belt through friction, while pulley lagging improves grip and minimizes belt slippage.
- Material Loading: Materials, products or components are introduced onto the carrying surface through manual loading, hoppers, chutes or suitable feeding arrangements.
- Material Conveying: Carrying rollers support both the belt and its load, helping maintain smooth, balanced and controlled movement.
- Discharging: When the belt reaches the discharge end, the conveyed material leaves the belt and is transferred to another machine, process or collection area.
- Return Cycle: After discharge, the empty belt moves along the lower return section over return rollers and travels back toward the loading point.
- Continuous Operation: These components together create a Belt Conveyor System capable of providing continuous material transportation and can incorporate automated tracks used to transport materials and goods wherever required.
Types of Industrial Belt Conveyor
As Industrial Belt Conveyor Manufacturers, Suppliers, Dealers and Exporters in Pune, Maharashtra, we manufacture and supply different conveyor arrangements according to application and material-handling requirements.
- Flat Belt Conveyor: A flat conveying surface provides stable transportation for cartons, components, packages and finished products used across assembly, manufacturing and packaging operations.
- Roller Bed Conveyor: Rollers installed below the belt provide additional support and reduce conveying resistance, making this configuration appropriate for heavier loads and extended conveying distances.
- Modular Belt Conveyor: Interconnected plastic modules form a durable conveying surface that can be cleaned and replaced section by section, making it suitable for continuous industrial production. Depending on the application, arrangements may include Belt Conveyor; Modular Belt Conveyor; Roller Conveyor; Slat Chain Conveyor.
- Cleated Belt Conveyor: Cleats fixed across the belt provide additional grip and help retain products when conveying at an incline. An Industrial Inclined Belt Conveyor is useful for moving materials between different floor levels.
- Curved Belt Conveyor: A curved arrangement allows the conveying direction to change while utilizing available floor space efficiently in manufacturing, sorting and packaging environments.
- Troughed Belt Conveyor: Inclined carrying rollers form a trough-like belt profile that helps retain and transport loose bulk material in larger quantities.
- Wire Mesh Conveyor: Metal mesh belts are capable of operating under elevated temperatures, cooling conditions and other demanding processing environments, making them suitable for drying, baking and thermal applications.
- Sidewall Belt Conveyor: Corrugated sidewalls and cleats provide material containment during steep-angle conveying, allowing efficient vertical or space-saving transportation.
- Vacuum Conveyor: Suction applied through openings in the belt helps hold lightweight products against the conveying surface, making this arrangement useful for films, sheets and delicate components.
- Magnetic Conveyor: Magnetic components located below the conveying surface attract and move ferrous parts, metal pieces and scrap, including applications requiring inclined conveying.
These conveyor configurations can be developed into a Belt Industrial Conveyor System based on product characteristics, load, speed, layout, available space and production requirements.
Technical Specifications of Industrial Belt Conveyor
As Industrial Belt Conveyor Suppliers, Manufacturers, Dealers and Exporters in Pune, Maharashtra, we provide customizable specifications to meet diverse industrial handling requirements.
| Parameter | Specification |
|---|---|
| Belt Width | 300–2,400 mm, customizable |
| Belt Thickness | 6–30 mm, application-based |
| Carcass Material | EP, NN or Steel Cord |
| Number of Plies | 2–8 plies |
| Tensile Strength | 315–3,150 N/mm |
| Top Cover | 3–15 mm |
| Bottom Cover | 1.5–10 mm |
| Cover Grade | Abrasion, heat, oil or fire resistant |
| Rubber Hardness | 60–75 Shore A |
| Conveyor Length | 1 m to 500+ m, customizable |
| Belt Speed | 0.5–2.5 m/s, application-based |
| Drive Power | 1 HP to dual 200 kW drives |
| Operating Temperature | -40°C to +80°C for standard belts |
| Configuration | Flat, inclined or customized |
| Standards | IS 1891, DIN 22102, ISO 340 and RMA guidelines |
The required industrial belt conveyor capacity, belt dimensions, conveying rate and drive power depend on material properties and desired throughput. For suitable belt conveyor power calculation, parameters including conveyor length, material load, belt weight, inclination, resistance, friction and operating conditions need to be considered. Proper evaluation of Belt conveyor parts and functions is also important when determining the appropriate conveyor arrangement.
Key Features of Industrial Belt Conveyor
As Industrial Belt Conveyor Dealers, Suppliers, Manufacturers and Exporters in Pune, Maharashtra, we provide conveyor systems incorporating practical features for dependable industrial material movement.
- Strong Industrial Construction: Heavy-duty frames, dependable belts and suitable drive components provide stable performance for demanding conveying applications.
- Requirement-Based Configuration: Belt dimensions, conveyor length, belt construction, operating speed and drive mechanisms can be selected according to the application.
- Effective Load Transportation: The equipment is configured to handle products and bulk materials according to the specified industrial belt conveyor capacity and is ideal for medium-load material handling where applicable.
- Versatile Conveyor Layout: Flat, inclined, cleated and specially configured conveyors can be designed according to production-line requirements and available installation space.
- Automation Integration: Sensors, controllers and other automation devices can be incorporated into the Belt Conveyor System to coordinate material movement and production processes.
Benefits of Industrial Belt Conveyor
As Industrial Belt Conveyor Exporters, Dealers, Suppliers and Manufacturers in Pune, Maharashtra, we provide conveying systems intended to improve workflow, material movement and operational productivity.
- Efficient Material Transfer: Continuous belt operation allows products and materials to move steadily between process points while reducing repetitive manual transportation.
- Better Production Coordination: Conveyors can link individual workstations and processes to establish a systematic and continuous material flow.
- Lower Manual Handling: Automated conveying reduces the need for repeated lifting, carrying and transferring of products between different stages.
- Flexible Operating Conditions: Belt speed, conveyor dimensions and load-handling arrangements can be adapted to suit different production requirements.
- Dependable Service Life: Appropriate material selection, durable construction and correctly selected components contribute to consistent operation with manageable maintenance needs.
Applications of Industrial Belt Conveyor
As Industrial Belt Conveyor Suppliers, Exporters, Dealers and Manufacturers in Pune, Maharashtra, we offer conveying solutions for multiple industrial material-transfer requirements.
- Manufacturing Industries: Used for moving raw materials, workpieces, components and finished products between various manufacturing operations.
- Packaging Lines: Enables the continuous transfer of cartons, boxes, containers and packaged products through filling, sealing, labelling and packing processes.
- Assembly Plants: Supports organized transportation of parts and completed assemblies between individual workstations.
- Warehousing & Distribution: Helps move packages and products through storage, sorting, picking, staging and dispatch operations.
- Food Processing: Suitable conveyor configurations can support hygienic product transportation when appropriate belt materials and sanitary construction are selected. Options such as SS Inclined Conveyor - Modular Belt can be considered for suitable requirements.
- Mining & Bulk Material Handling: Heavy-duty conveyor arrangements can continuously transport bulk materials across suitable conveying distances.
- Pharmaceutical Industries: Provides controlled movement of packaged products, components and materials between processing, inspection and packaging areas.
- Logistics & Material Transfer: Facilitates consistent transportation of goods across industrial facilities where repetitive product movement is required.
Why Choose Us?
- Quality-Focused Engineering: We select appropriate materials, dependable components and established engineering methods to manufacture an Industrial Belt Conveyor intended for stable and consistent industrial operation.
- Customized Application Design: We assess the conveying requirement and configure dimensions, belt selection, capacity, drive system and layout to develop a Belt Industrial Conveyor System appropriate for the customer's production process.
- Technical Assistance: We support installation, maintenance, troubleshooting and technical requirements to help customers maintain reliable conveyor operation across different industrial applications.
S Cube Engineering & Automation is leading Industrial Belt Conveyor Manufacturers, Suppliers, Dealers and Exporters in Pune, Maharashtra. We design and deliver customized conveyor solutions based on specific industrial handling and production needs. Our systems combine robust construction, practical engineering and application-oriented customization for consistent material movement and reliable operation. From standard conveyor layouts to specialized configurations, we serve diverse manufacturing and material-handling applications with suitable solutions. Our focus remains on quality, operational efficiency, dependable performance and responsive technical support. Contact us for customized conveyor solutions and further details.
Location