Food Grade Belt Conveyor

Food Grade Belt Conveyor Manufacturers in Pune - S Cube Engineering
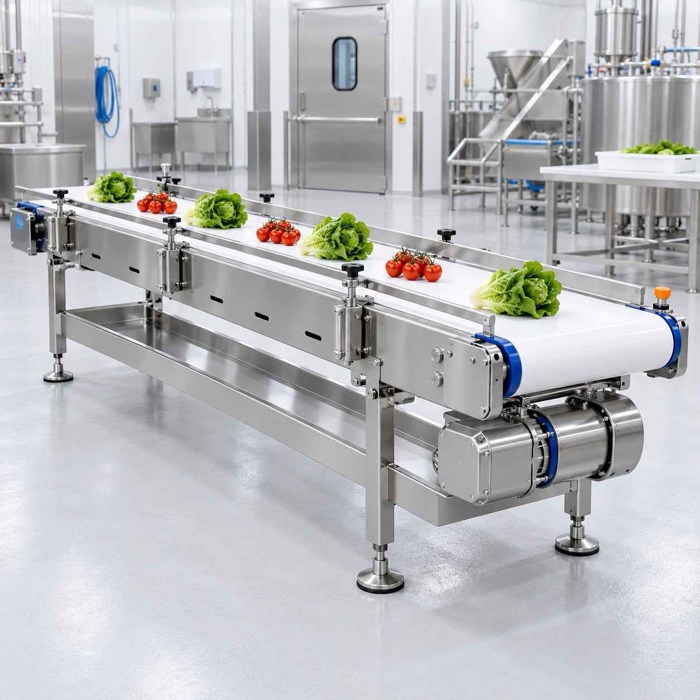
S Cube Engineering & Automation is leading Food Grade Belt Conveyor Manufacturers, Suppliers, Dealers and Exporters in Pune, Maharashtra. We provide dependable Food Grade Belt Conveyor solutions designed for hygienic and efficient movement of products across food-processing and packaging lines.
Our conveying systems are engineered with practical design principles, quality-oriented construction and application-specific customization to accommodate different product dimensions, conveying speeds and plant layouts. We offer competitive solutions while focusing on consistent performance and responsive service support.
Our Food Processing Conveyor Belt solutions facilitate smooth and continuous product transportation, while Stainless Steel Food Grade Belt Conveyor configurations offer a robust option for applications requiring enhanced hygiene and durability. From selecting and configuring the conveyor to installation and technical guidance, we provide complete conveying solutions for contemporary food-handling and packaging facilities.
What Is a Food Grade Belt Conveyor and How Does It Support Hygienic Food Handling?
A Food Grade Belt Conveyor is a hygienically designed conveying system used to move edible products safely and efficiently between various stages such as processing, inspection, sorting and packaging. It incorporates food-suitable belt materials and cleanable construction intended for demanding food-processing environments.
By providing controlled and consistent product movement, the conveyor helps streamline production, minimize unnecessary manual handling and maintain an uninterrupted workflow. A continuous conveying system developed for food-processing applications can effectively connect multiple production stages while supporting organized and efficient product transportation.
Working Principle of Food Grade Belt Conveyor
The conveyor operates through a motor-powered belt arrangement that carries food products steadily from one point to another. Hygienic materials and accessible construction help make the system suitable for food-processing applications.
- Power Transmission: An electric motor coupled with a gearbox drives the pulley and transfers rotational power to the conveyor belt, enabling consistent operation of the Food Grade Conveyor Belting.
- Belt Movement: The powered drive pulley engages with the belt and moves it continuously along the conveyor frame, allowing products to travel at a controlled and predetermined speed.
- Product Conveying: Food products are placed on the conveying surface and transported smoothly toward subsequent processing, inspection, sorting or packaging stations.
- Return Movement: Following product discharge, the unloaded belt moves back through the return section over suitable support rollers, completing the continuous conveying loop.
- Belt Tensioning: An appropriate tensioning arrangement keeps the belt correctly tensioned to reduce slipping, sagging and tracking-related problems. Tensionless food grade belting fits loosely can be considered for applications where the conveyor configuration and working conditions allow such an arrangement.
- Hygienic Construction: Food-compatible materials combined with stainless-steel construction provide a cleanable conveying arrangement appropriate for Food Grade and HACCP Conveyor Belts applications. Depending on the applicable requirements, suitable components may be Approved by FDA/ USDA / HACCP.
- Easy Sanitation: Open and accessible construction allows convenient cleaning, inspection and maintenance, supporting hygienic conditions during regular food-processing operations.
Types of Food Grade Belt Conveyor
As Food Grade Belt Conveyor Manufacturers, Suppliers, Dealers and Exporters in Pune, Maharashtra, we offer application-oriented conveying equipment with customized configurations for food handling and processing requirements.
Types by Belt Material
- Polyurethane (PU) Conveyor Belt: Pu Conveyor Belt Food Grade solutions offer good resistance to oils, fats and moisture. They can be used in suitable meat, dairy, bakery and other food-processing applications. Polyurethane Volta Beltings Food Grade PU Belts are also used as terminology for suitable polyurethane food-grade belt solutions.
- Polyvinyl Chloride (PVC) Conveyor Belt: A PVC Food/ Material Conveyor Belt offers a practical and economical conveying option for dry foods, packaged goods, sorting operations and general material transportation. A PVC Food Grade Conveyor Belt can be selected when its characteristics meet the specific product and process requirements.
- Silicone Conveyor Belt: Silicone belts provide a smooth and non-stick conveying surface along with useful heat resistance. They can be suitable for sticky food products and selected applications involving elevated processing temperatures.
- PTFE Coated Fiberglass Belt: PTFE-coated fiberglass belts offer high thermal stability and non-stick characteristics, making them appropriate for selected baking, drying, heating and dehydration processes.
- Food-Grade Rubber Belt: Food-grade rubber belts provide durable conveying performance and useful resistance to moisture and oils, making them suitable for selected agricultural and food-processing duties.
- Plastic Modular Belt: Modular Belt Conveyor Systems utilize interlocking plastic belt sections that can simplify maintenance while offering drainage and airflow advantages in appropriate wet-processing, washing and cooling applications.
Types by Structure and Layout
- Flat Belt Conveyor: A flat belt conveyor offers a level conveying surface for horizontal product transportation and is commonly used for sorting, inspection, processing and packaging applications. The FOOD GRADE PU FLAT BELT CONVEYOR configuration can be selected where a flat conveying arrangement and suitable PU belt properties are required.
- Inclined / Z-Type Conveyor: A Mild Steel Inclined food grade Belt conveyor can transfer products between different elevations while making effective use of available production-floor space.
- Wire Mesh Conveyor: Wire mesh belts allow improved airflow and heat circulation around conveyed products, making them suitable for selected baking, cooling, drying and thermal food-processing operations.
Technical Specifications of Food Grade Belt Conveyor
As Food Grade Belt Conveyor Suppliers, Manufacturers, Dealers and Exporters in Pune, Maharashtra, we provide customizable specifications for varied food-processing requirements.
| Parameter | Typical Specification |
|---|---|
| Conveyor Type | Horizontal, inclined or declining configuration |
| Frame Material | SS 304 / SS 316L stainless steel |
| Belt Material | PU, TPU, food-grade PVC or approved rubber |
| Belt Width | 200–1,500 mm; customized as required |
| Conveyor Length | 2–20 m; application-specific customization available |
| Operating Temperature | Approx. –30°C to +80°C, depending on belt material |
| Load Capacity | Up to 50–100 kg/m; heavy-duty designs available |
| Drive System | Geared motor, drum motor or suitable motorized drive |
| Motor Rating | Typically 0.5–2 HP, based on conveyor load and speed |
| Belt Speed | Fixed or variable speed as per application |
| Belt Colour | White or blue; blue options support easy visual inspection |
| Belt Jointing | Thermo-spliced or hygienic mechanical jointing as applicable |
| Surface Finish | Smooth, cleanable and suitable for hygienic processing areas |
| Cleaning Design | Open-frame and accessible construction for convenient washdown |
| Control System | Manual, electrical or automation-integrated control |
| Customization | Width, length, height, speed, belt type and layout can be customized |
Key Features of Food Grade Belt Conveyor
As Food Grade Belt Conveyor Dealers, Suppliers, Manufacturers and Exporters in Pune, Maharashtra, we emphasize hygienic design, dependable operation and configurations matched to the specific production requirement.
- Hygienic Construction: Stainless-steel frames and suitable food-contact belt materials create a durable and cleanable conveying surface for food-processing environments.
- Application-Specific Belt Selection: We can configure Food Grade Thermoplastic Belts, PU, PVC and other appropriate belt materials according to the conveyed product, operating conditions and process requirements.
- Smooth Product Handling: Controlled belt travel allows products to move steadily between process stages while helping minimize unnecessary product movement or disturbance.
- Easy Cleaning & Maintenance: Accessible conveyor construction facilitates routine cleaning, inspection and maintenance, supporting hygienic and reliable operation.
- Customized Configuration: Conveyor dimensions, elevation, speed, belt selection and overall layout can be modified to suit individual manufacturing-line requirements.
Benefits of Food Grade Belt Conveyor
As Food Grade Belt Conveyor Exporters, Dealers, Suppliers and Manufacturers in Pune, Maharashtra we develop conveying solutions around hygiene, production efficiency and dependable product transportation.
- Improved Production Efficiency: Continuous conveying maintains a steady flow of products and reduces avoidable manual transportation between different production stages.
- Enhanced Food Hygiene: Appropriate food-contact materials and cleanable construction support hygienic product movement and practical food-processing requirements.
- Reduced Manual Effort: Automated conveying reduces repetitive manual movement and allows production personnel to concentrate on essential processing and quality activities.
- Flexible Line Integration: Food Grade Belt Conveyor Systems can be arranged to connect processing, inspection, sorting and packaging equipment as part of an integrated production line.
- Reliable Long-Term Operation: Proper belt selection, suitable construction and application-focused engineering can contribute to dependable performance with practical maintenance requirements.
Applications of Food Grade Belt Conveyor
As Food Grade Belt Conveyor Suppliers, Exporters, Dealers and Manufacturers in Pune, Maharashtra, we supply conveying solutions for a broad range of food-processing, handling, inspection and packaging requirements.
- Bakery & Confectionery: Suitable conveyor arrangements can transport bread, biscuits, cakes, chocolates and other bakery products between processing and packaging stages.
- Dairy Processing: Hygienically designed conveyors can be incorporated into suitable dairy production, handling and packaged-product transportation applications.
- Meat & Poultry Processing: Appropriate belt and conveyor configurations support controlled transportation of processed products in designated hygienic handling areas.
- Fruit & Vegetable Processing: Conveyors can move washed, sorted, sliced, cut and prepared fruits and vegetables between different processing operations.
- Ready-to-Eat Foods: Food conveyors for bakery, confectionery, RTE, meat, poultry, seafood, and dairy applications can facilitate continuous product movement through interconnected production processes.
- Grain & Pellet Handling: A Food Grade Belt Conveyor for Grain and Pellet Handling System can provide controlled transportation for appropriate dry food materials and selected granular products.
- Food Packaging Lines: Conveyors can transfer pouches, trays, cartons, containers and other packaged goods toward inspection, labeling or packaging equipment.
- Sorting & Inspection: A stable conveying surface allows operators or inspection systems to perform product checking, sorting and quality-control activities efficiently.
For applications where enhanced hygienic construction and corrosion resistance are required, a Stainless Steel Industrial Food Grade Belt arrangement can offer a durable solution for food-processing and packaging environments.
Why Choose Us?
- Engineering Focused on Quality: We manufacture and supply food-conveying systems using suitable materials, proven engineering practices and application-oriented designs to deliver consistent and dependable industrial performance.
- Customized & Economical Solutions: We offer Food Grade Conveyor Belts ideal for conveying edible materials, with configurations developed according to the product characteristics, conveyor dimensions, production capacity, layout and specific operating conditions.
- End-to-End Technical Assistance: From selecting the appropriate conveyor and developing the required configuration to installation and after-sales technical support, we assist customers throughout the complete implementation process.
S Cube Engineering & Automation is well-known Food Grade Belt Conveyor Manufacturers, Suppliers, Dealers and Exporters in Pune, Maharashtra. We specialize in supplying customized Food Grade Belt Conveyor solutions developed for hygienic handling, smooth product movement and efficient production operations. Our engineered conveyor systems are designed to integrate effectively with food-processing and packaging lines while delivering consistent conveying performance. We combine suitable materials, practical engineering, customized configurations and quality-focused manufacturing to address varied application requirements. With competitive pricing and dependable technical assistance, we support customers with practical conveying solutions designed for efficient operation, reliable performance and lasting industrial value. Contact us for further details.
Location